What changes the pressure at the tool
Pressure falls as compressed air moves through a hose, tube, pipe, fitting, filter, or regulator. Friction against the inside wall and restrictions in the flow path create the loss.
Three variables have an especially visible effect:
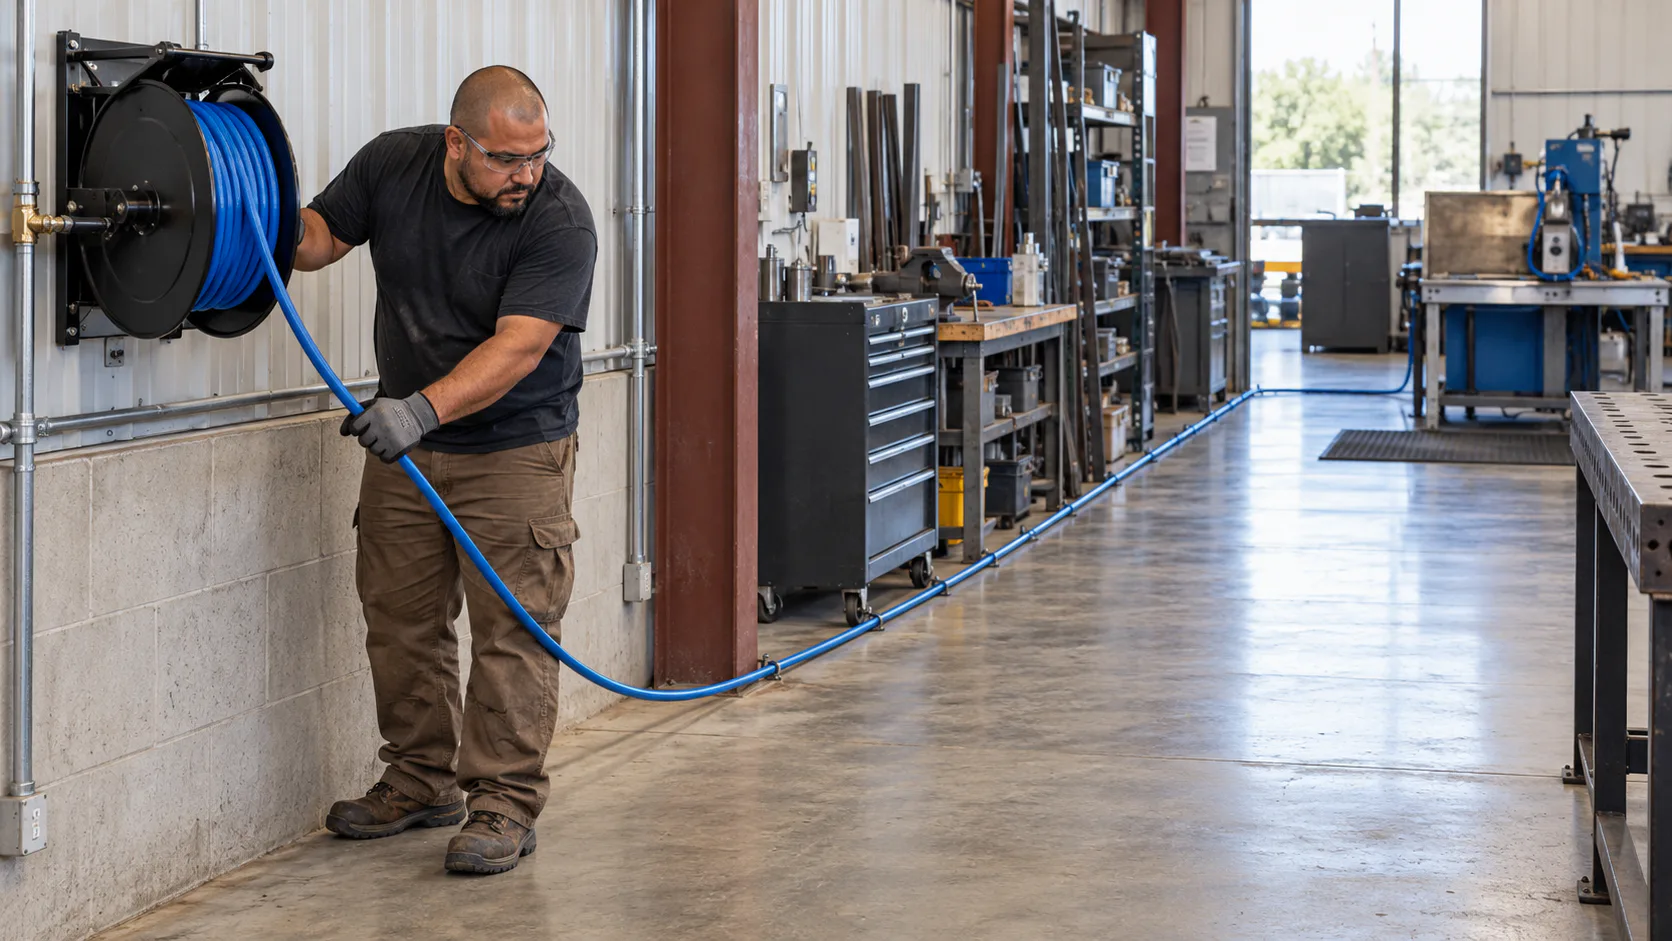
- Length: a longer run produces more pressure loss when the other conditions stay the same.
- Inside diameter: a smaller opening raises velocity and pressure drop.
- Airflow: a tool demanding more air produces a larger drop through the same line.
The pressure shown at the compressor is therefore not necessarily the pressure available at the tool while air is flowing.
How hose length changes pressure loss
Reelcraft's hose bulletin states that pressure loss is directly proportional to length. If a given hose loses 2 PSI over 50 feet under a particular set of conditions, the same hose at the same flow and inlet pressure would lose approximately 4 PSI over 100 feet. A 25-foot run would lose approximately 1 PSI.
EXAIR gives the same proportional rule for its Schedule 40 steel-pipe tables. One published example reports a 2.07 PSI drop through 100 feet of quarter-inch Schedule 40 pipe at 5 SCFM and 90 PSIG. For 50 feet of that same pipe at the same conditions, EXAIR says to use approximately half the table value, or about 1.0 PSI.
That number belongs to steel pipe with a 0.364-inch actual inside diameter. It is not a universal pressure-loss figure for a quarter-inch hose.
What the published steel-pipe table shows
EXAIR's table reports pressure drop in PSI for 100 feet of Schedule 40 steel pipe. It is useful here because it isolates the effect of flow and actual inside diameter. It is not presented as a hose-performance table.
| Free air | 1/4-inch Schedule 40 pipe, 0.364-inch actual ID | 3/8-inch Schedule 40 pipe, 0.493-inch actual ID |
|---|---|---|
| 1 SCFM | 0.11 PSI drop | 0 PSI drop* |
| 2 SCFM | 0.38 PSI drop | 0.08 PSI drop |
| 3 SCFM | 0.80 PSI drop | 0.18 PSI drop |
| 4 SCFM | 1.37 PSI drop | 0.30 PSI drop |
| 5 SCFM | 2.07 PSI drop | 0.45 PSI drop |
Conditions: 100 feet of Schedule 40 steel pipe at 90 PSIG line pressure. Note: the source table displays zero at its published precision; it should not be read as proof of no physical loss whatsoever.
At 5 SCFM, the table's quarter-inch pipe value is 2.07 PSI while its three-eighths-inch pipe value is 0.45 PSI. At 1 SCFM, the quarter-inch value is only 0.11 PSI. The same line becomes more restrictive as airflow rises.
Why inside diameter matters so much
EXAIR publishes a pressure-drop equation in which inside diameter appears to the fifth power in the denominator. With the other variables held constant, halving the inside diameter increases the calculated pressure drop by a factor of 32.
The same source explains a related flow effect. At equal air velocity, halving the inside diameter reduces flow to 25 percent. To move the same flow through that smaller opening, velocity would have to rise fourfold. That is why a small bore in one fitting can matter even when the hose itself is larger.
Use actual inside diameter, not the nominal thread or product size, when a source provides it.
A 3/8-inch hose is not the same as 3/8-inch tube
EXAIR explains that compressed-air hose is measured by inside diameter while tube is measured by outside diameter. In its comparison:
- 3/8-inch hose has a 0.375-inch inside diameter.
- 3/8-inch tube has a 0.25-inch inside diameter.
Using its pressure-drop relationship, EXAIR calculates that the tube produces 7.6 times the pressure drop of the hose under the example's other fixed conditions.
Nominal size can also hide close matches across different materials. EXAIR lists a quarter-inch NPT Schedule 40 pipe at 0.364 inch inside and a three-eighths-inch compressed-air hose at 0.375 inch inside. The labels differ, but the actual openings are close.
EXAIR consequently recommends moving one size larger than the recommended pipe size when compressed-air hose is used. That is EXAIR's sizing recommendation for the conditions it discusses, not a substitute for the tool and hose manufacturers' instructions.
Quick connects and other restrictions
A hose can be correctly sized while a fitting, filter, regulator, or valve becomes the narrowest part of the path.
EXAIR shows one quarter-inch quick-disconnect example whose internal opening measures close to 0.192 inch, much smaller than its nominal NPT connection. In EXAIR's Super Air Knife example, that fitting cannot support the required volume and causes a pressure drop.
The 0.192-inch measurement belongs to the specific fitting shown in that source. Quick connects with the same nominal connection can have different internal geometries, so inspect the published bore or flow rating for the actual fitting rather than assigning this measurement to the whole category.
Reelcraft also cautions that its hose curves are guides. Hose inside-diameter tolerance, fitting type, and orifice restrictions affect actual discharge. Its bulletin says temperature can change friction loss by 20 percent and bends can increase it by 50 percent.
Reelcraft's worked hose-sizing example
Reelcraft provides a practical example for a production paint spray gun requiring 8 CFM of free air at 80 to 100 PSI. The example uses Reelcraft's 50-foot hose curve with a 90 PSI inlet.
On the bulletin's hose curve, the quarter-inch inside-diameter hose reaches a 15 PSI pressure loss at that demand. Reelcraft says the quarter-inch hose cannot be recommended and selects the next larger size, a three-eighths-inch inside-diameter hose.
This example is useful because it deals with hose rather than steel pipe. Reelcraft describes its chart values as calculated general-reference figures and says tool manufacturers' recommendations should govern. A different hose construction, length, inlet pressure, fitting set, or tool demand requires its own check.
A practical diagnostic sequence
When a pneumatic tool feels weak at the end of a line, check the complete flow path:
- Find the tool's published airflow and required operating pressure.
- Measure the hose run and record the hose's actual inside diameter.
- Check the bore or flow rating of quick connects, filters, regulators, swivels, and valves.
- Look for unnecessary bends, kinks, damaged hose, and undersized sections.
- Measure pressure at the tool while it is flowing air, following the manufacturer's test procedure.
- Compare the result with a pressure-drop table or curve for the actual hose or pipe material and size.
Do not compensate for a restrictive line by raising pressure beyond the tool, hose, fitting, or compressor limits. Follow the manufacturers' instructions and have a qualified person review permanent plumbing, electrical work, or a multi-tool installation.
The same-pressure comparison guide explains how to keep tool demand and compressor output conditions aligned. You can also use the matcher for exact CFM-labelled records before accounting for the downstream hose and fittings.
Sources checked
- Pressure Drop / Flow Rate Charts and Graphs | Reelcraft, checked 2026-10-07.
- How to Calculate and Avoid Compressed Air Pressure Drop | EXAIR, checked 2026-10-07.
- Pipe Pressure Drop | EXAIR, checked 2026-10-07.
- Pipe sizing articles | EXAIR, checked 2026-10-07.
Technical tables and curves apply only to their stated conditions. Recheck current specifications for the exact hose, pipe, fittings, tool, and compressor before changing a system.